
H550 Powder System Unveiled
Engineering breakdown of the high-throughput selective laser sintering architecture and integrated breakout post-processing ecosystem.
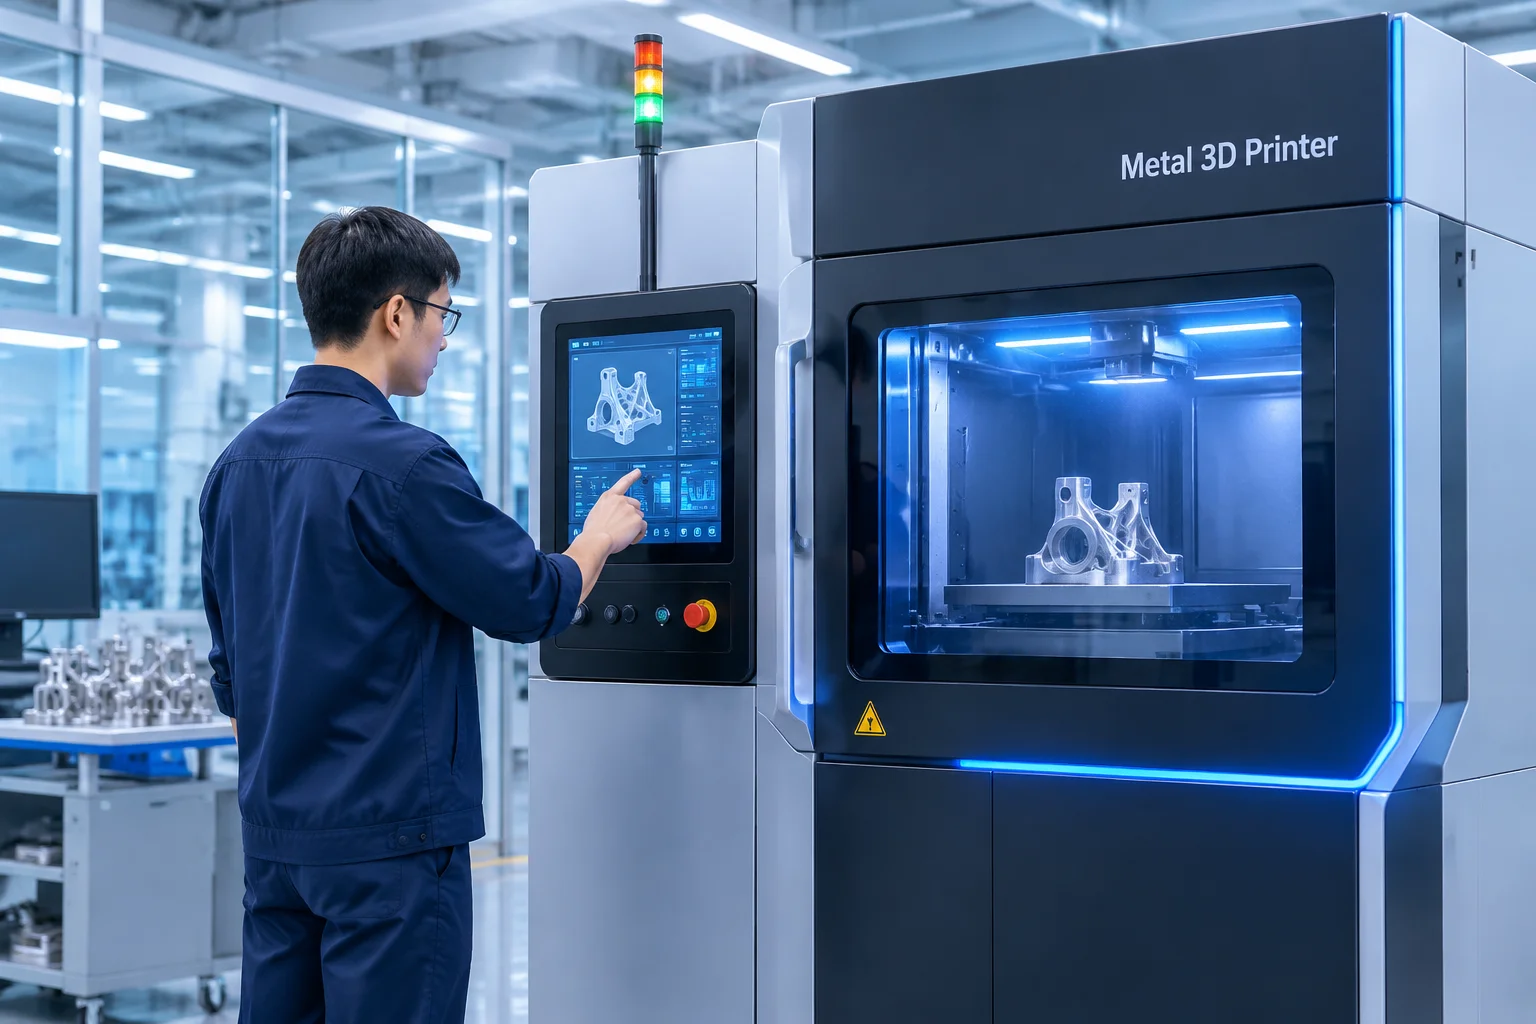
High-Throughput Selective Laser Sintering with Autonomous Material De-Caking
The H550 powder platform introduces a continuous dual-laser scanning array alongside an automated breakout post-processing chamber designed for serial additive manufacturing. By combining an expanded 550 x 550 x 600 mm build volume with closed-loop nitrogen recycling and dynamic thermal balancing across eight heated zones, the system addresses previous throughput bottlenecks in nylon PA11 and PA12 serial production. Its companion breakout unit automates part extraction and powder de-caking, reducing manual handling cycles while preserving material refresh ratios down to twenty percent virgin stock.
Machine Parameters and Operational Limits
| Parameter | Value / Technical Scope |
|---|---|
| Usable Build Volume | 550 × 550 × 600 mm (181.5 L) |
| Optical Array | Dual 100W CO₂ Lasers with Dynamic 3-Axis Galvos |
| Scan Velocity | Up to 15.0 m/s per individual beam |
| Chamber Atmosphere Control | Inert N₂ atmosphere with O₂ below 0.1% |
| Surface Thermal Uniformity | ±1.2°C across active bed via 8-zone PID heating |
| Companion Station Function | Automated breakout, ultrasonic sieving, and reconditioning |
- Dual optical scanning heads halve layer exposure intervals while cross-sync calibration eliminates overlap seams across split fields.
- Integrated pneumatic conveyance channels unsintered powder directly into an ultrasonic screener without exposing operators to particulate clouds.
- Eight independently monitored infrared zones eliminate thermal drop-offs at perimeter boundaries, maintaining dimensional fidelity across high-density vertical nests.
Multi-Zone Radiant Heating and Closed-Loop Powder Handling
Thermal stability across a large 550 mm square build plane requires real-time thermal compensation. The H550 addresses this with an array of multi-wavelength pyrometers feeding dynamic thermal calculations directly into the radiant heater bank. By maintaining layer surface deviations within narrow limits, parts avoid curling or differential shrinkage throughout the extended vertical build cycle.
After sintering completes, the self-contained build canister rolls into the breakout enclosure along dedicated guide rails. Ultrasonic vibration modules dislodge cake powder without damaging thin mechanical walls, while pneumatic collection tubes feed the material straight into an integrated inert reconditioning unit for automated mixing.
Maintaining rigorous thermal symmetry throughout high-density powder beds is essential for dimensional repeat accuracy. The H550 synchronizes continuous optical scanning with an automated handling ecosystem that minimizes operator handling risks.